Case study
High-Volume Fastener Manufacturer
Chhatrapati Sambhajinagar MIDC
“The machines stopped jamming on the night shift. That alone paid for the grade change.”
01
The challenge
The customer runs a bank of multi-spindle automatics producing small turned fasteners in high volume, including an unattended night shift. Cost per piece on this kind of work is dominated by machine time, not by the price of a kilogram of steel.
Running standard free cutting bar, they were losing production to chip-related stoppages. Long swarf was wrapping around tooling and workpieces, and a jam on an unattended shift meant the machine stood idle until the morning.
Tool changes were frequent, and surface finish off the tool was inconsistent enough that some parts needed a secondary operation they had not planned for.
They were also carrying bar feed faults caused by straightness variation — a bowed bar will not index reliably through a collet.
02
What we changed
Grade supplied
EN1A PBLead-added EN1A — the fastest machining grade we produce.
Lead acts as an internal lubricant at the cutting edge
We moved the high-speed automatic work to EN1A PB. The lead content acts as an internal lubricant at the cutting zone, working alongside the sulphide inclusions that break the chip, giving both shorter chips and a lower friction cut.
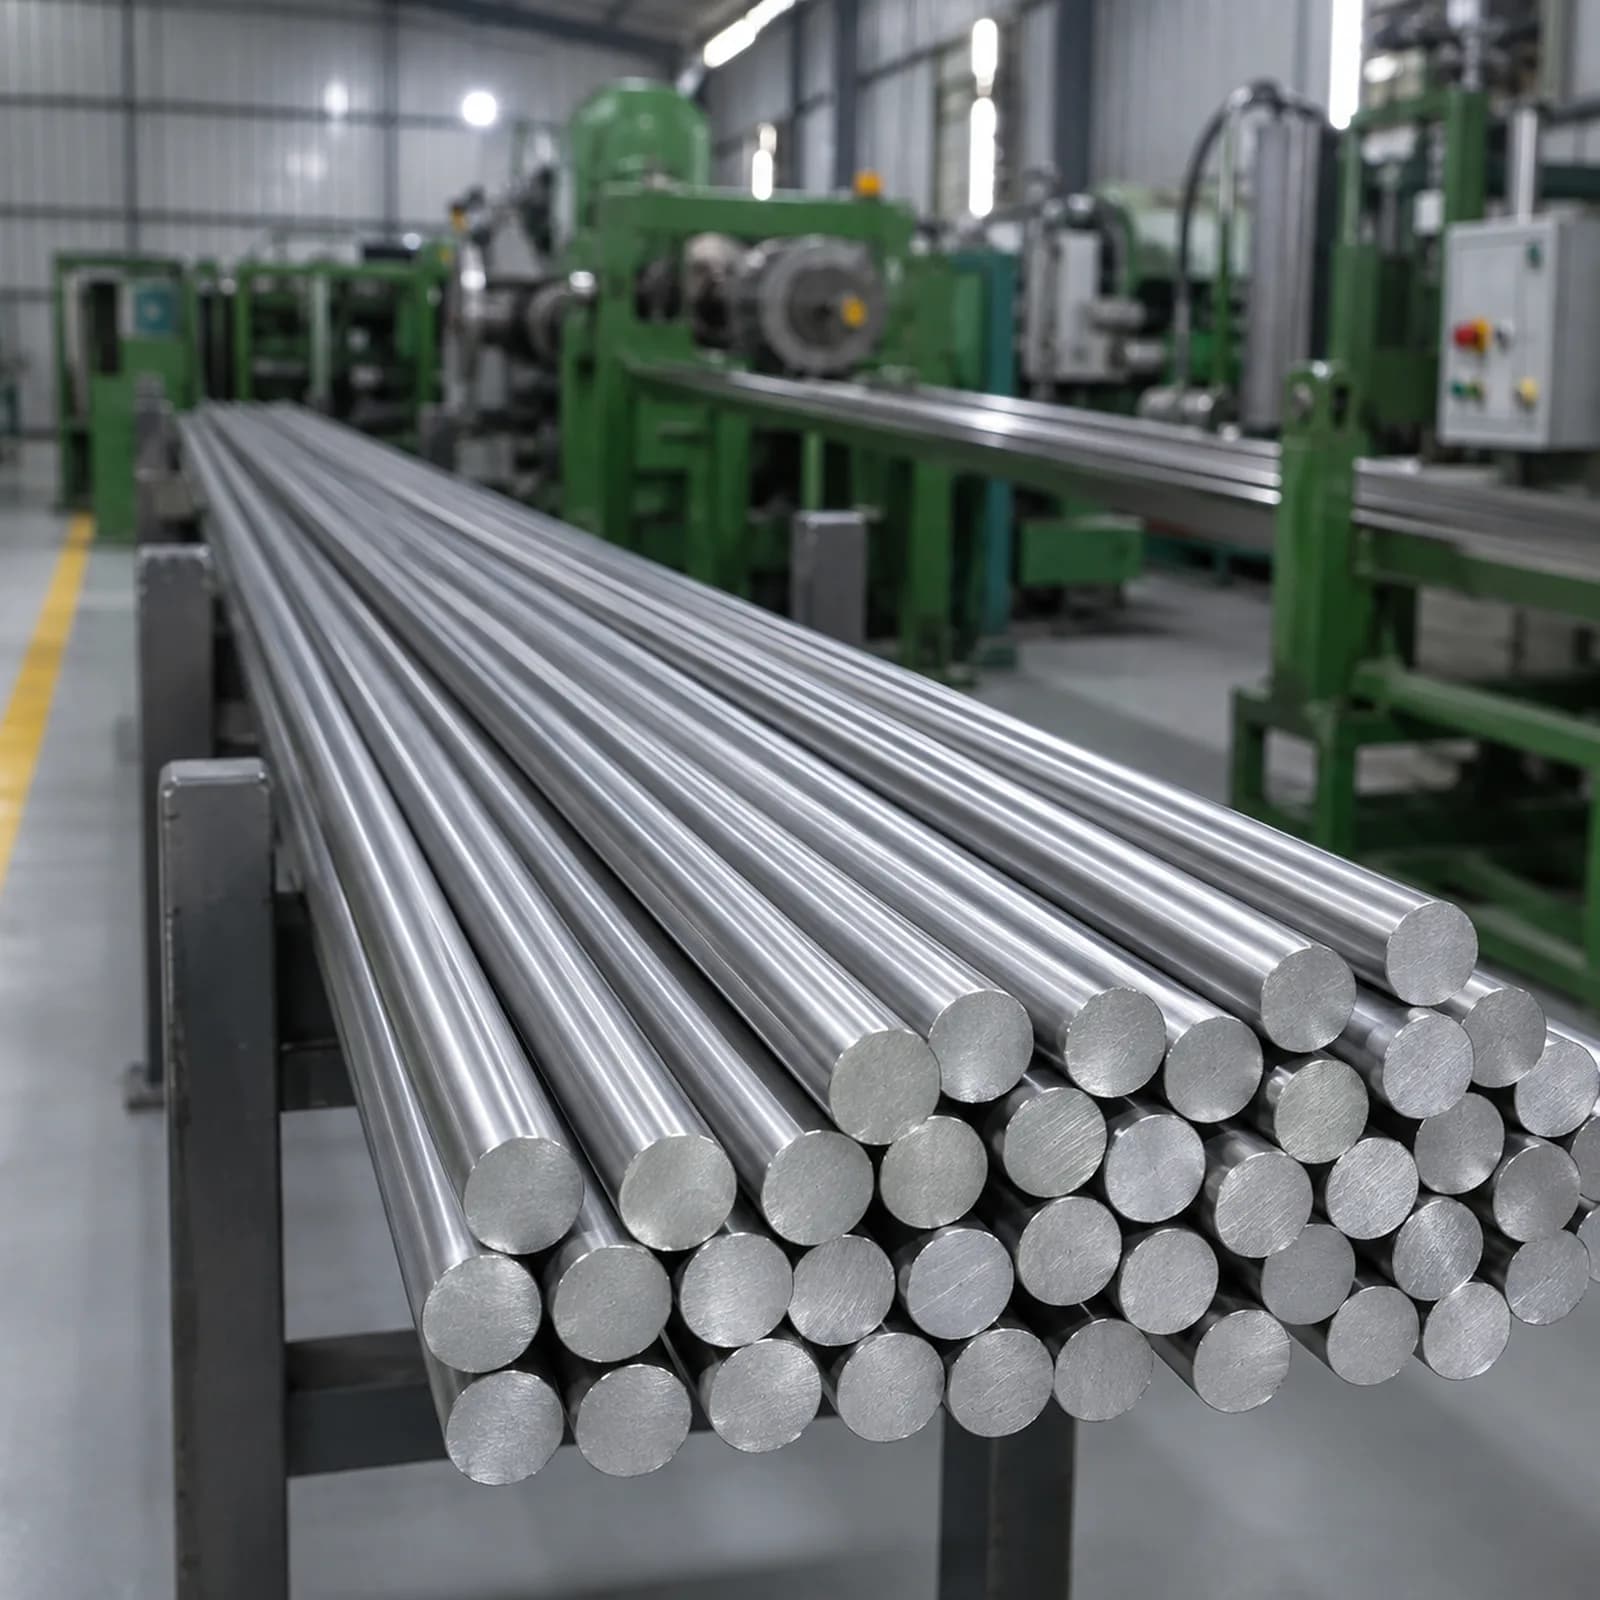
Hex and round were drawn to h10 with straightness controlled as a monitored process parameter rather than an incidental outcome, and cut to the length their bar feeders were set for.
Bundles were tagged and scheduled so the shop floor could identify grade and size at a glance, removing the risk of feeding the wrong bar into a set machine.
03
The result
- Chip-related stoppages on the unattended night shift substantially reduced
- Longer tool life between changes on the high-speed automatics
- Better surface finish off the tool — a planned secondary operation removed on part of the range
- Bar feed faults reduced through controlled straightness and consistent cut length
- Higher material cost per kilogram offset several times over by recovered machine hours
Results described here are those reported by the customer for their process and product. Outcomes on your parts depend on your design, your machining and your heat treatment, and are not guaranteed by the material alone.
Chemical composition and mechanical properties shown are as per the applicable standard and are indicative. Actual values for your consignment are certified in the Mill Test Certificate supplied with each dispatch. Available sizes and tolerances are confirmed at the time of enquiry.
Discuss your requirement
Tell us what is happening on your line. If the answer is a different grade, we will say so — including when it is one we do not stock.